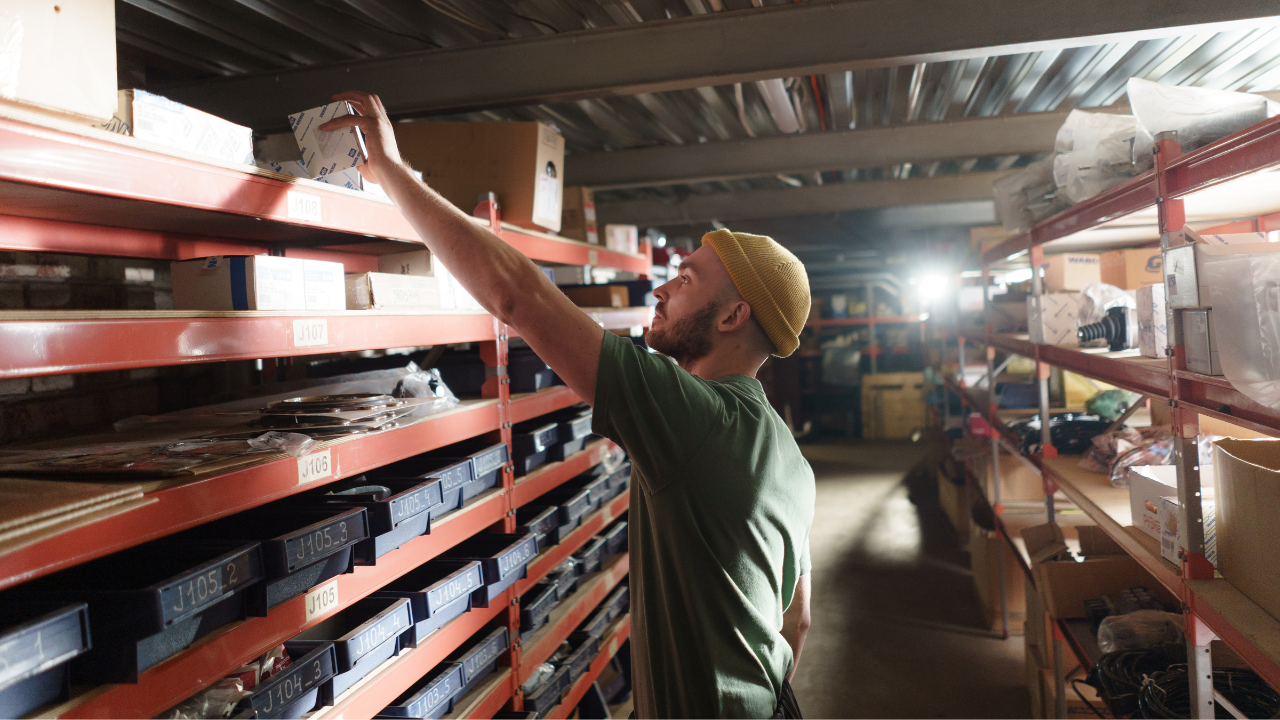
In any organization there are many departments that must work closely with other departments. One vital partnership is maintenance and the maintenance storeroom – nothing is more important than getting the right parts at the right time to achieve a high level of maintenance effectiveness.
While this partnership is vital, it is difficult to develop and maintain because it requires a high level of discipline and determination by both parties. This article covers the dual responsibilities required to achieve success.
In my experience, many maintenance storeroom operations are ineffective. The focus is often placed on security: keeping the building locked, not allowing maintenance people to physically look for parts, and generally preventing losses. Sometimes the storeroom goals are completely out of sync with maintenance’s goals.
For example, maintenance storerooms may focus on reducing inventory without understanding the consequences. I’ve even seen instances where storerooms report to purchasing (stores and purchasing are very different functions) which in turn reports to a corporate “procurement” organization. A structure that makes maintenance storerooms “organizationally remote” from its customer will always create service problems.
To develop a picture of an effective maintenance storeroom, it’s good to start with these three principles:
Maintenance storerooms should have complete business processes, standards, systems, facilities and staff to control and protect maintenance materials from the time they enter the premises until the time they are used on a maintenance job. This should include stocked materials, “zero-stock” catalogue materials, direct purchases and some special parts that may be stored outside of the storeroom building.
Storerooms should make it as easy as possible for maintenance people to find, select, obtain and return the materials they need while always maintaining a high level of security. | Check out my next article to learn how to control materials returned to stores
Materials should be stored and handled so that they will always be in a condition that will meet reliability goals when they leave storeroom control.
Following these principles, the “internal supply chain” for maintenance materials, with responsibilities, will look like this:
The implications of such a process are significant and require maintenance and the maintenance storeroom to work closely together to achieve success. For example, if the storeroom is to stage materials for maintenance work, as shown, maintenance MUST advise the storeroom of all the materials needed (a product of planning) and tell stores when it will be used (a product of scheduling).
Without proper planning and scheduling, staging material will be very difficult and certainly wasteful. This requirement means that the maintenance storeroom effectiveness is dependent on the discipline with which operations and maintenance can schedule maintenance work, and requires that scheduled work should be planned in detail.
Storerooms should support maintenance by providing the following services:
A simple and robust way for maintenance people at all levels to find materials, supported by good naming standards, a comprehensive integrated “stock and non-stock” catalogue and willing help from storeroom staff when needed, all supported by a highly functional computer system.
A well-managed “free issue” system for small parts.
A suitable physical facility adequately staffed to securely store, protect, control, retrieve, stage, and deliver all stocked items and all direct purchased items.
A secure location and facilities for staging “work order kits” for at least two weeks of non-shutdown maintenance work if a weekly work scheduling process is in use.
A suitable physical facility to securely store, protect, control, retrieve and deliver all materials for planned shutdowns.
A simple process to accept returned items and ensure that they are fit for re-stocking.
Record the location and movement of parts that are stored outside of the maintenance storeroom, with input from maintenance and operations people who are responsible for these parts.
Sound basic inventory-management systems to immediately re-stock items that have reached their re-order point, replace items that have reached their shelf life and manage other basic inventory functions.
Maintain an integrated catalogue of stocked and appropriate non-stock items, based on a naming standard that uses the same terminology as used by maintenance people.
Investigate stock-outs and advise maintenance if they appear to be caused by equipment problems (e.g. increase usage) or by using maintenance stock for projects.
Because the maintenance storeroom has the business processes to control the movement of materials, include all objects that are used by maintenance. This could include special tools and maintenance manuals, for these items it is especially important that the process is very simple, for example using a “tool tag” system and not the computer system.
Finally, to support maintenance and the maintenance storeroom in managing materials and tools, managers must ensure that the operation has a very high level of security and that any instances of theft of company property are dealt with in a manner that will strongly discourage any further theft.
If the maintenance “Statement of purpose” is “to provide our operating partners with a physical plant which, if operated correctly, will continue to meet all goals including production, quality, safety, and the environment at the lowest possible total cost over the long term” the storeroom Statement of Purpose should be “to provide our Maintenance partners with all the materials they need at the right time and the right place and in a condition to support reliability goals, all at the lowest possible cost over the long term”.
Don Armstrong is the President of Veleda Services – Maintenance Management Consulting and Training. Don is an experienced professional engineer and has managed a number of large maintenance departments over the years. In addition, he has successfully instituted new planning and scheduling processes, maintenance standards, and safety programs into maintenance departments.
The last of the ‘baby boomer’ generation are now retiring from the workplace. As they walk out of the door of your business for the last time, they are taking with them a lifetime's experience from old-school apprenticeship programmes to a lifetime of fault diagnosis and learning in the ‘university of life.’ That experience is what helped your business grow, become successful, and kept your customers happy and returning with repeat orders! So, what can be achieved in the time before valued employees retire for knowledge capture and knowledge transfer so your business can maintain momentum?
The last of the ‘baby boomer’ generation are now retiring from the workplace. As they walk out of the door of your business for the last time, they are taking with them a lifetime's experience from old-school apprenticeship programmes to a lifetime of fault diagnosis and learning in the ‘university of life.’ That experience is what helped your business grow, become successful, and kept your customers happy and returning with repeat orders! So, what can be achieved in the time before valued employees retire for knowledge capture and knowledge transfer so your business can maintain momentum?
With today's limited internal resources, it's tough to transform machine maintenance from reactionary to preventive, and ultimately proactive, despite the obvious upsides in higher overall equipment efficiency (OEE), better process control and lower total cost. Outsourcing this requirement to a third-party specialist, however, is a cost-effective alternative, according to companies that have crunched the numbers.
With today's limited internal resources, it's tough to transform machine maintenance from reactionary to preventive, and ultimately proactive, despite the obvious upsides in higher overall equipment efficiency (OEE), better process control and lower total cost. Outsourcing this requirement to a third-party specialist, however, is a cost-effective alternative, according to companies that have crunched the numbers.
Besides being the central hub for maintenance, the storeroom also provides functions that are absolutely critical to the maintenance operation. These functions are so important that when the storeroom is operating in a best practices mode, the rest of the maintenance operation can excel – the storeroom is the enabler. Put another way, if the storeroom is run improperly (such as poor inventory accuracy, parts unavailable when needed due to poor replenishment and procurement practices, etc), the rest of the maintenance operation has no chance of achieving high service levels of equipment availability and reliability.
Besides being the central hub for maintenance, the storeroom also provides functions that are absolutely critical to the maintenance operation. These functions are so important that when the storeroom is operating in a best practices mode, the rest of the maintenance operation can excel – the storeroom is the enabler. Put another way, if the storeroom is run improperly (such as poor inventory accuracy, parts unavailable when needed due to poor replenishment and procurement practices, etc), the rest of the maintenance operation has no chance of achieving high service levels of equipment availability and reliability.
The new general manager at Doe Run’s South-east Missouri Mining and Milling Division determined that inaccurate and incomplete maintenance data was a major contributing factor preventing effective management of maintenance costs. Management then decided to obtain the necessary knowledge and tools which would allow implementation and operation of an effective maintenance management program. The company chose to pilot a program at one of the mines, and depending on its success, the program would be expanded to other areas within the division.
The new general manager at Doe Run’s South-east Missouri Mining and Milling Division determined that inaccurate and incomplete maintenance data was a major contributing factor preventing effective management of maintenance costs. Management then decided to obtain the necessary knowledge and tools which would allow implementation and operation of an effective maintenance management program. The company chose to pilot a program at one of the mines, and depending on its success, the program would be expanded to other areas within the division.
The single greatest challenge facing managers in the developed countries of the world is to raise the productivity of knowledge and service workers. This challenge, which will dominate the management agenda for the next several decades, will ultimately determine the competitive performance of companies. Even more important, it will determine the very fabric of society and the quality of life in every industrialized nation.
The single greatest challenge facing managers in the developed countries of the world is to raise the productivity of knowledge and service workers. This challenge, which will dominate the management agenda for the next several decades, will ultimately determine the competitive performance of companies. Even more important, it will determine the very fabric of society and the quality of life in every industrialized nation.
Another trite phrase has the answer: The weakest link in a chain is the strongest because it can break it. Preventative and routine maintenance models help alleviate downtime and boost overall production. The most popular method is Total Productive Maintenance (TPM). TPM assigns the responsibility for preventative and routine maintenance to the same people who operate that individual equipment. This puts the people most familiar with the machine in charge of its care.
Another trite phrase has the answer: The weakest link in a chain is the strongest because it can break it. Preventative and routine maintenance models help alleviate downtime and boost overall production. The most popular method is Total Productive Maintenance (TPM). TPM assigns the responsibility for preventative and routine maintenance to the same people who operate that individual equipment. This puts the people most familiar with the machine in charge of its care.
You need to read this article on maintenance management of PLCs. Why? Because the PLCs (Programmable Logic Controllers) are the brains of your operation. When the PLC is not functioning properly, lines shut down, plants shutdown, even city bridges and water stations could cease to operate. Thousands to millions could be lost by one little PLC in an electrical panel that you never even knew existed. But most importantly, damage to machine and personnel could result from improper maintenance management of your company’s PLCs.
You need to read this article on maintenance management of PLCs. Why? Because the PLCs (Programmable Logic Controllers) are the brains of your operation. When the PLC is not functioning properly, lines shut down, plants shutdown, even city bridges and water stations could cease to operate. Thousands to millions could be lost by one little PLC in an electrical panel that you never even knew existed. But most importantly, damage to machine and personnel could result from improper maintenance management of your company’s PLCs.
Lorem ipsum dolor sit amet, consectetur adipiscing elit. Nullam rhoncus, odio eget elementum volutpat, enim risus vulputate mauris, et luctus augue massa et sapien. Lorem ipsum dolor sit amet, consectetur adipiscing elit. In efficitur mi in erat lacinia tincidunt. Cras vulputate nec nulla vitae pretium. Integer porttitor mattis justo at fringilla. Donec eleifend massa turpis, at auctor mi pulvinar sit amet. Cras ut turpis id arcu fringilla gravida.