Standard Practices vs. Right Practices
Few answers to machine relubrication questions are black and white. But, it is reasonable to state that relubrication work practices, in a practical sense, are either right or wrong. There is no middle ground!
Recently, a mechanical supervisor at a seminar that I led went out of his way to argue against efforts to redo his lubrication practices. He stated that his site had devoted much time to developing and executing high-quality lubrication practices. He explained that there were well-defined practices keyed into the CMMS system; the work was routinely scheduled, issued, completed and logged; and the process was in good working order. He could produce stats to show this.
I asked him to describe a typical bearing relubrication practice by the key issues he would expect to find. He identified the machine, the type of work to be conducted (lubricate a group of bearings), the planned frequency and the product that would be used (a name-brand, general-purpose grease). That sounded good, but it wasn’t. A debate quickly developed among plant personnel over whether the grease noted for the described work was, in fact, the type that was actually in use. It wasn’t, but within the ensuing debate I argued that there was no one exclusive product that should be selected, and that the lubricant in use was acceptable for the application.
Uh-oh. Is that a contradiction? Not quite. While the points identified reflected a degree of correctness, these are types of details that must be fulfilled in order for every scheduled activity to occur (machine, frequency, materials required, description of work required). It was a bare minimum of details cobbled together for someone to complete the task of coding lubrication PM activities to the CMMS. It was of no surprise at all that the designated lubricant was not the product in use and that there was:
- no definition of the required volume;
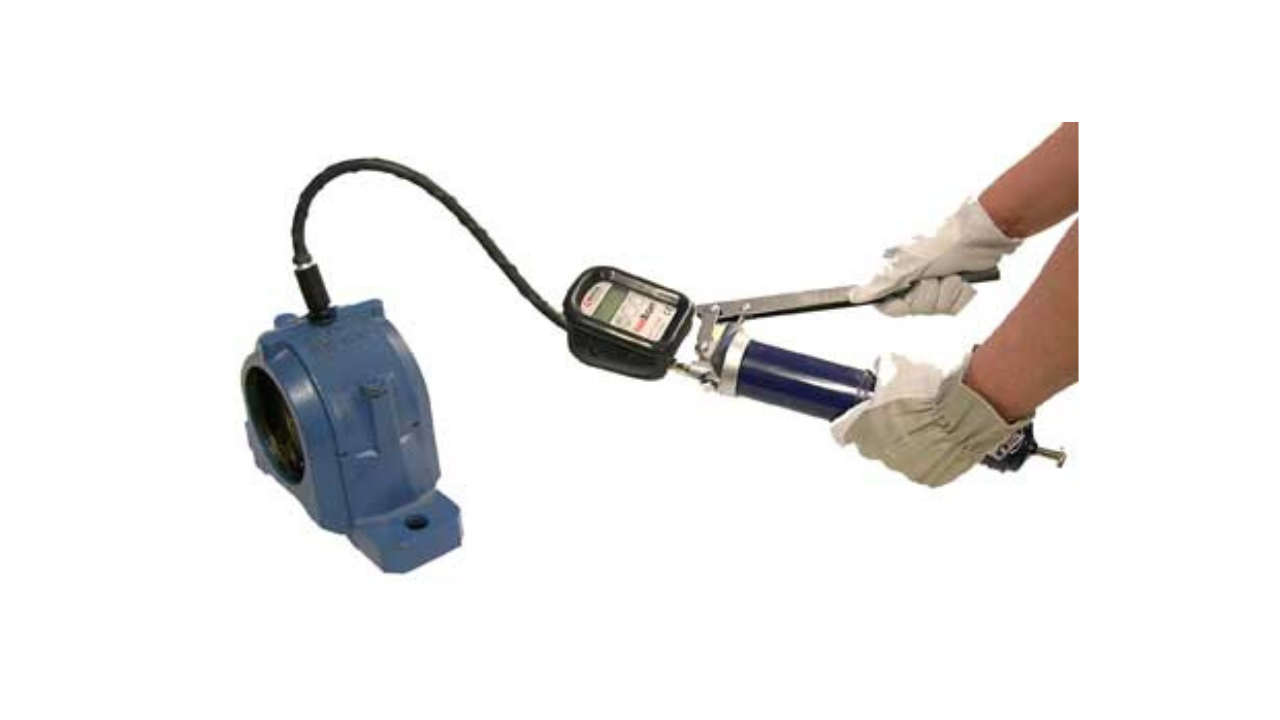
- no definition of the tool (grease gun, by volumetric ratio) to be used to assure the correct volume;
- no definition of conditions to observe with which to judge whether the designated volume would, in practice, be correct; and,
- no definition of the required running state of the machine at the time of the work order execution.
These and other details determine if the work practice is right or wrong.
Back to the first point of this column. Often, the perception of quality derives from the presence of a practice. The practice exists, therefore it is right. In reality, a scheduled task is often passed off as a standard regardless of rightness. This disconnect occurs because the relubrication portion of the CMMS deployment follows a troubled model. A flawed practice is coded into a program. This doesn’t make the practice functional.
That leads to my second point: Why does a CMMS development team invest long hours to replicate a broken lubrication plan? Eventually, someone decides that the paper-based program is good enough and that precious development hours should be spent elsewhere. This default decision becomes the design decision around which the future is built. If the decision is anything short of a decision to implement a best practice, the practices are wrong.
How do you know where you stand? Here are two simple options:
1) Benchmark the existing practice against a best practice: The technical gap analysis (product type selection, viscosity grade, frequency, volume, contamination control effectiveness, oil health management, oil analysis effectiveness) will identify any room for improvement.
2) Follow the money: Review the purchase history of lubricants and lubricated components (bearings, sprockets, chains, reducers, hydraulic components) to gather clear feedback on the quality of the existing plan. Deduct replacements for extenuating circumstances. Whatever purchases remain reflect the program’s real value. These dollar values are the tip of the iceberg of potential savings from precision lubrication.
In the earlier example, the supervisor judged the practices to be right because they were part of a system designed for routine relubrication. The work was available to be scheduled, the work could be tracked, and tracking statistics could be used as evidence that the work was completed. However, he could not objectively measure the relative quality of the practices in place. There was no objective measure of whether the work was right or wrong. The plan is right only when it is accurate, thorough, efficient and available in black and white.
Related Articles
A number of common mistakes are made in selecting, scoping and carrying out lubrication PM tasks and intervals. I have outlined four common "wrongs" with respect to lube PM optimization, which can, with some effort and guidance, be turned into four "rights."
A number of common mistakes are made in selecting, scoping and carrying out lubrication PM tasks and intervals. I have outlined four common "wrongs" with respect to lube PM optimization, which can, with some effort and guidance, be turned into four "rights."
See More
So what is going wrong with the lubricant and bearings in our pumps? We do not get a service life any where near those numbers. It turns out that most bearings fail prematurely for only two reasons: High heat that caused the lubricant to "varnish" and then form "coke" that will introduce solids into the lubricant, and contamination of the lubricant by water, moisture, and solids.
So what is going wrong with the lubricant and bearings in our pumps? We do not get a service life any where near those numbers. It turns out that most bearings fail prematurely for only two reasons: High heat that caused the lubricant to "varnish" and then form "coke" that will introduce solids into the lubricant, and contamination of the lubricant by water, moisture, and solids.
See More
This project, like so many others, had a humble beginning. About five years ago, after returning from a routine sales call to the smelter where a representative was selling synthetic and specialty greases, he challenged the authors to develop a series of lubricants that he could sell to the aluminum industry. In a discussion with a group of maintenance people at the smelter, he was told that if his company could develop longer lasting lubricants and protect equipment better than the current product, they would buy from him.
This project, like so many others, had a humble beginning. About five years ago, after returning from a routine sales call to the smelter where a representative was selling synthetic and specialty greases, he challenged the authors to develop a series of lubricants that he could sell to the aluminum industry. In a discussion with a group of maintenance people at the smelter, he was told that if his company could develop longer lasting lubricants and protect equipment better than the current product, they would buy from him.
See More
Most, if not all, companies use CMMS systems to oversee their maintenance activities. From home-grown systems to complete ERP systems, leveraging technology allows companies to more efficiently and effectively manage their maintenance, repair and operations activities. So as a core maintenance function, surely routine, lubrication-related preventive and predictive activities such as regreasing motor bearings, taking oil samples, and executing oil top-offs and inspections belong in the CMMS system like any other maintenance task, right?
Most, if not all, companies use CMMS systems to oversee their maintenance activities. From home-grown systems to complete ERP systems, leveraging technology allows companies to more efficiently and effectively manage their maintenance, repair and operations activities. So as a core maintenance function, surely routine, lubrication-related preventive and predictive activities such as regreasing motor bearings, taking oil samples, and executing oil top-offs and inspections belong in the CMMS system like any other maintenance task, right?
See More
Adding the correct amount of lubrication at each re-lubricating interval is essential to achieve maximum bearing life. An incorrect re-lubrication quantity, whether it's too much or too little, can actually decrease bearing life.
Adding the correct amount of lubrication at each re-lubricating interval is essential to achieve maximum bearing life. An incorrect re-lubrication quantity, whether it's too much or too little, can actually decrease bearing life.
See More
ASSALUB has introduced a new technology to help track manual greasing. This technology can help improve your lubrication program and ensure the practices you aim to implement are being completed. The LubeRight is a computer aided manual greasing system that offers the following advantages when compared to traditional manual greasing.
ASSALUB has introduced a new technology to help track manual greasing. This technology can help improve your lubrication program and ensure the practices you aim to implement are being completed. The LubeRight is a computer aided manual greasing system that offers the following advantages when compared to traditional manual greasing.
See More
Machinery and Equipment MRO interviewed three oil and lubrication specialists to uncover industry trends that are important to suppliers and users alike. They were asked to consider factors that significantly influence decision-making on more easily protecting equipment, and to share insights on what's new, what holds value and provides improvements, as well as what helps solve common problems.
Machinery and Equipment MRO interviewed three oil and lubrication specialists to uncover industry trends that are important to suppliers and users alike. They were asked to consider factors that significantly influence decision-making on more easily protecting equipment, and to share insights on what's new, what holds value and provides improvements, as well as what helps solve common problems.
See More