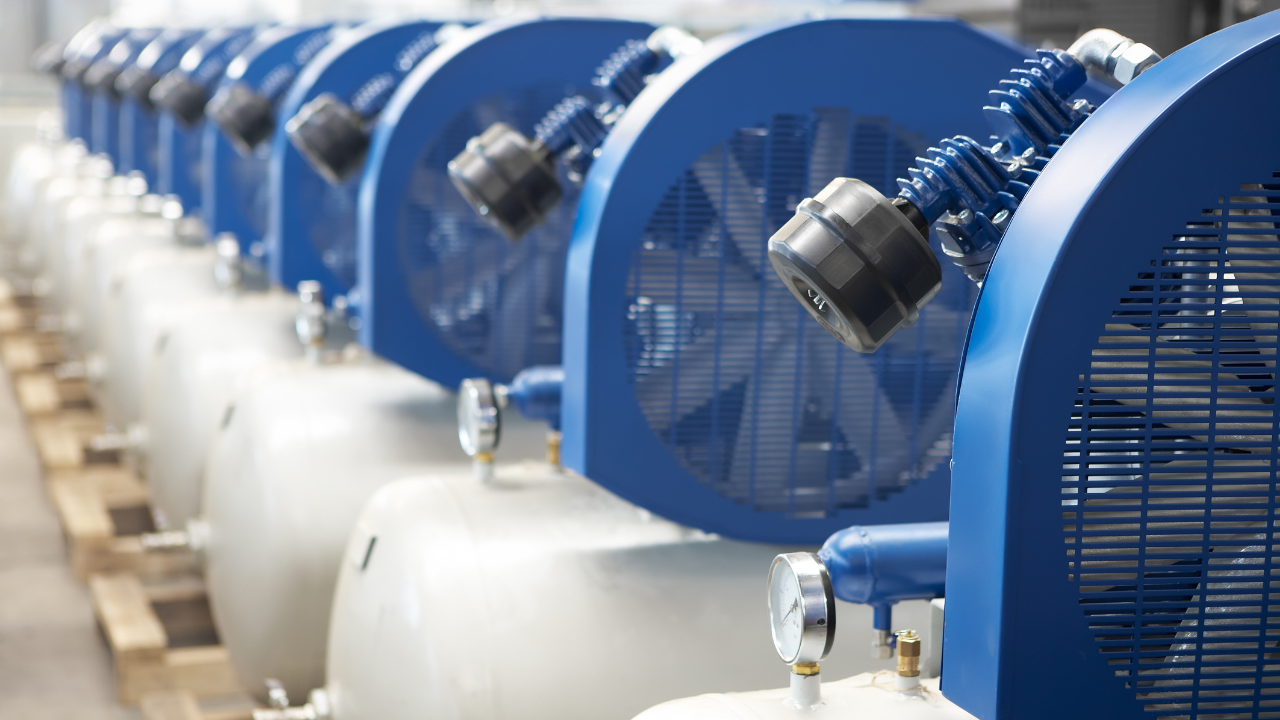
The article is intended to provide a few tips for blower maintenance to plant maintenance professionals in reducing the downtime and increasing the reliability of blowers.
Generally the apparent reasons for blower failure are:
Failure of Bearings
High Vibrations
The most common reason for these is unbalance of the rotor assembly. It is noted that if balancing of the rotor is checked/rectified as and when time permits, especially during the Shutdowns/Turnarounds, a marked improvement in the performance shall be visible in blower performance.
This is easier said than done. Due to various constraints this exercise is often omitted. For such cases it will always be useful to at least do static balancing of the assembly on site. This is an easy exercise and the time requirements are also very minimal.
The engineer is much at ease in case it is a N.D.E. bearing, which has failed, and can get the machine on line after replacing the N.D.E. Bearing and realigning the drive.
This job is complicated and becomes time consuming in case the bearing does not come out with help of a puller, and in that case at times gas cutting of inner race has to be done. This also aggravates the chances of damaging the shaft, which would result in a major maintenance work.
In the case of D.E. bearing failure, over and above the above mentioned consideration a new jobs comes in, that is removal of the coupling half. Normally as recommended couplings are interference fits, and removing them is a very time consuming job. At times it has been noted that many plant engineers keeping this difficulty in mind go in for a slight clearance fit for coupling halves. Though no engineer would admit freely, the same procedure for increasing the clearance slightly is followed for bearing fitting also, so as to ease the removal of these after failure. Though it is not a good practice but the pressure that a plant engineer has to face for handing over the breakdown machine normally forces him to adopt these practical techniques.
The best solution for these kinds of situations is to go in for split type bearings in blowers. The introduction of Split Bearing eliminates totally all the above stated problems and the maintenance time required comes down drastically in case of failures. Also the performance of Split bearings is in no way inferior to normal bearings. Only adverse criterion why the OEM’s do not recommend this bearing is the high cost of this type of bearings.
It is recommended that the plant engineer should at least study the cost benefits of conversion to this type of a bearing and normally he shall find it to be a more economic choice. It is always advisable to contact the manufacturer of the bearing for designing and recommending the best selection for the given drive.
It shall be noted that after following the above two recommendations, that is balancing of the rotor and changing of the bearing types, the operational and maintenance performance improvement of the said blower would be quite visible.
The one factor which shall help in even better performance of the blower is proper coupling selection. It is again noted that the OEM normally selects the coupling based on economy principles and the couplings generally recommended are like: Spring type coupling, Gear type Coupling, Tyre couplings, etc. These couplings are good from the point of economy but require constant maintenance in form of greasing or wear and tear replacements. This invariably also affects the performance of the blower. In a case it was noted that the axial vibration generated was as a result of spring type coupling, which is very poor in absorbing such vibrations.
It is recommended that the plant engineer should replace these types of couplings by all metallic, flexible high performance couplings. These couplings have the distinct advantages in form of:
Practically no maintenance is required.
Very good in control of vibrations due to better characteristics.
Energy conservation as these have less transmission losses.
It is felt that incorporating the above modifications and practices in a blower drive should give a plant engineer relief from maintaining the blowers regularly.
Air receivers store compressed air and are used to temporarily satisfy fluctuations in plant air demand. There are other benefits of a wet receiver such as cooling and cleaning the air before it enters the air treatment equipment. Storage benefits highlighted below apply to all compressor control types. Understanding best practices for compressor storage for a lubricated trim compressor with load/unload controls is critical for optimized performance.
Air receivers store compressed air and are used to temporarily satisfy fluctuations in plant air demand. There are other benefits of a wet receiver such as cooling and cleaning the air before it enters the air treatment equipment. Storage benefits highlighted below apply to all compressor control types. Understanding best practices for compressor storage for a lubricated trim compressor with load/unload controls is critical for optimized performance.
This article will briefly examine this evolution and highlight modern developments in protecting cooling water systems. Environmental issues related to industrial wastewater discharge are also influencing this evolution.
This article will briefly examine this evolution and highlight modern developments in protecting cooling water systems. Environmental issues related to industrial wastewater discharge are also influencing this evolution.
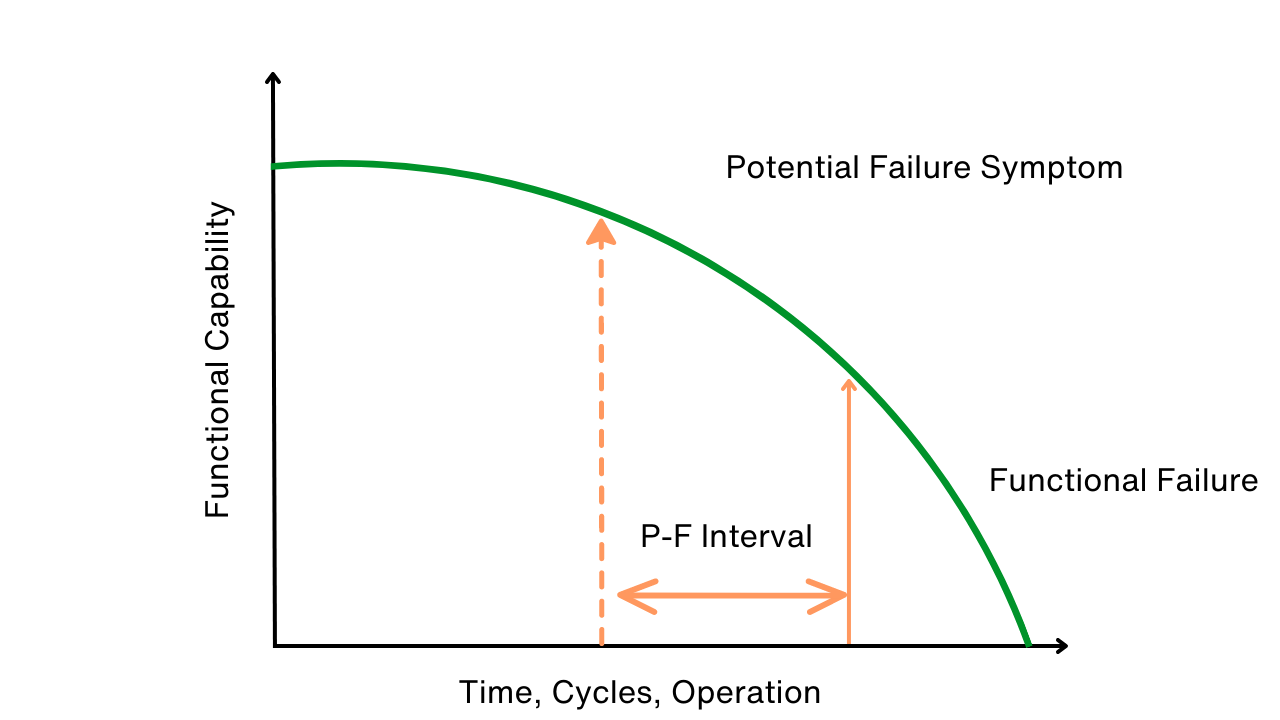
The potential-to-functional failure interval (P-F interval) is one of the most important concepts when it comes to performing Reliability-Centered Maintenance (RCM). Remarkably, the P-F interval is also one of the most misunderstood RCM concepts. The failure mode analysis becomes even more complicated when you are dealing with several P-F intervals for one failure mode. This paper will help clarify the P-F interval and the decision-making process when dealing with multiple P-F intervals.
The potential-to-functional failure interval (P-F interval) is one of the most important concepts when it comes to performing Reliability-Centered Maintenance (RCM). Remarkably, the P-F interval is also one of the most misunderstood RCM concepts. The failure mode analysis becomes even more complicated when you are dealing with several P-F intervals for one failure mode. This paper will help clarify the P-F interval and the decision-making process when dealing with multiple P-F intervals.
Such a question often comes up when it is time to recondition a mechanical seal: We use several different brands of mechanical seals in my plant. When a pump is taken out of service, we usually send the seal back to the original seal manufacturer for reconditioning. One of my suppliers has offered to recondition all of my seals, regardless of brand. Is this a good idea? Most process plant maintenance departments return their used mechanical seals to the original seal manufacturer (or Seal OEM) for reconditioning.
Such a question often comes up when it is time to recondition a mechanical seal: We use several different brands of mechanical seals in my plant. When a pump is taken out of service, we usually send the seal back to the original seal manufacturer for reconditioning. One of my suppliers has offered to recondition all of my seals, regardless of brand. Is this a good idea? Most process plant maintenance departments return their used mechanical seals to the original seal manufacturer (or Seal OEM) for reconditioning.
If you are currently running a vibration monitoring program in-house or outsourcing it to a consultant, before you potentially throw any more money in the toilet, you really need to audit your vibration monitoring program and ask yourself if you are getting any value out of it. If you do not know what benefits you are getting from a vibration monitoring program, you are probably not getting any benefits at all!
If you are currently running a vibration monitoring program in-house or outsourcing it to a consultant, before you potentially throw any more money in the toilet, you really need to audit your vibration monitoring program and ask yourself if you are getting any value out of it. If you do not know what benefits you are getting from a vibration monitoring program, you are probably not getting any benefits at all!
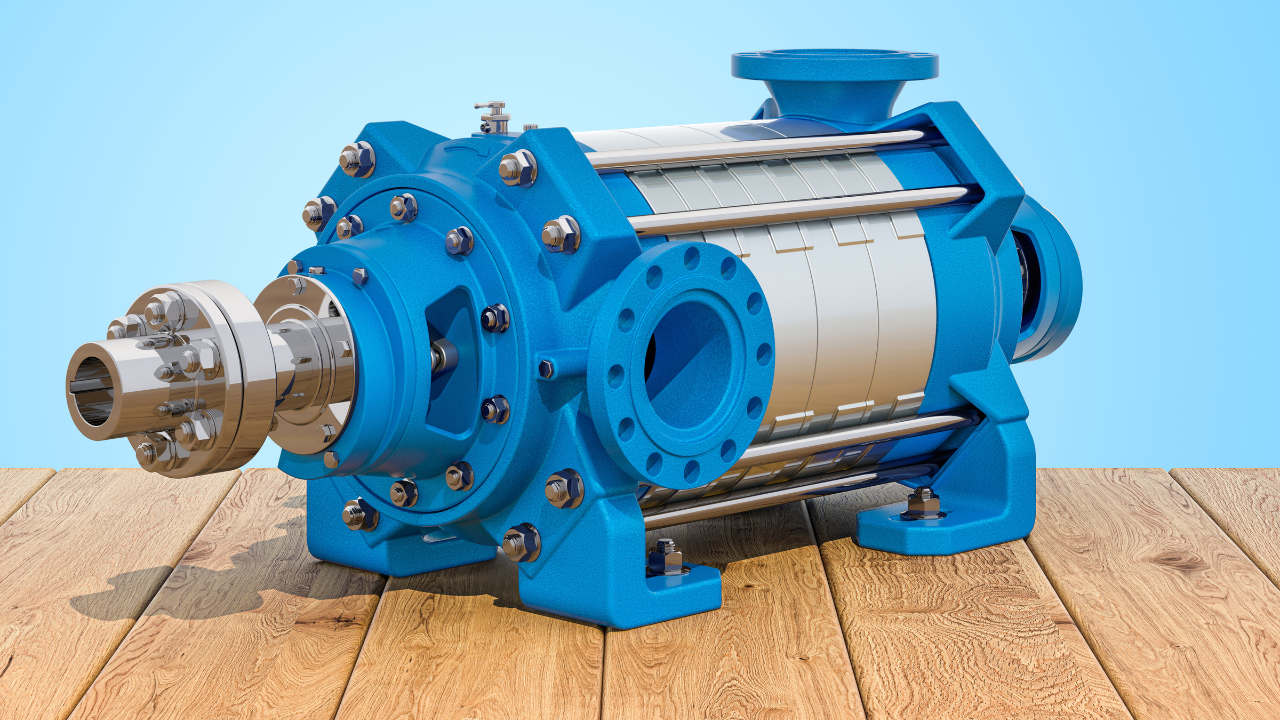
The fact of the matter is that there are three types of problems mostly encountered with centrifugal pumps: design errors, poor operation, poor maintenance practices. The present article is being presented in 3 parts: covering all aspects of operation, maintenance, and troubleshooting of centrifugal pumps.
The fact of the matter is that there are three types of problems mostly encountered with centrifugal pumps: design errors, poor operation, poor maintenance practices. The present article is being presented in 3 parts: covering all aspects of operation, maintenance, and troubleshooting of centrifugal pumps.
Proper asset care is critical to ensure that equipment is available to meet production schedules, support process flows and comply with environmental, health, safety, and regulatory requirements. Asset care is the execution of the most cost effective control strategy to address the predominant failure modes of that particular asset with its operating envelope. The intent of an asset care strategy is to provide the required asset utilization at the lowest life cycle cost while also ensuring the asset makes it to the budgeted end of life.
Proper asset care is critical to ensure that equipment is available to meet production schedules, support process flows and comply with environmental, health, safety, and regulatory requirements. Asset care is the execution of the most cost effective control strategy to address the predominant failure modes of that particular asset with its operating envelope. The intent of an asset care strategy is to provide the required asset utilization at the lowest life cycle cost while also ensuring the asset makes it to the budgeted end of life.